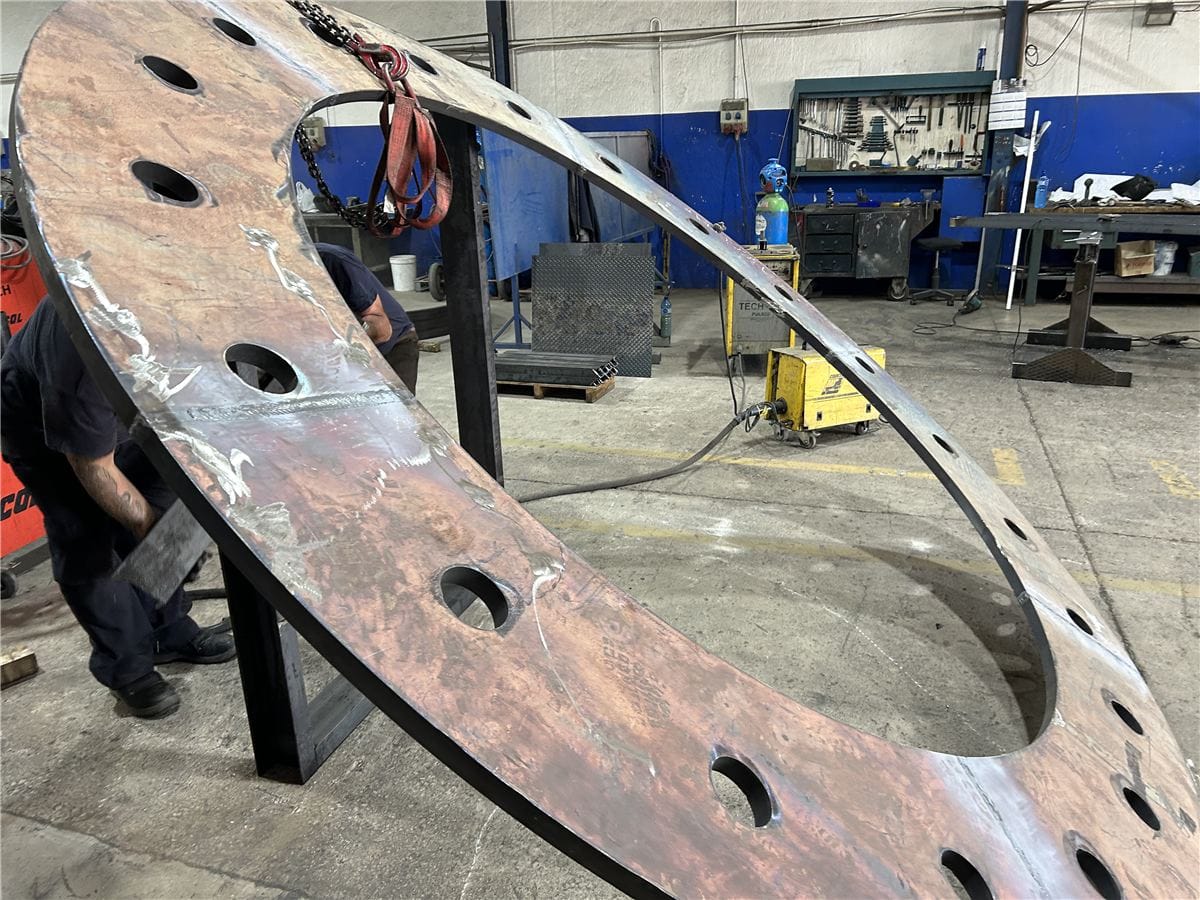
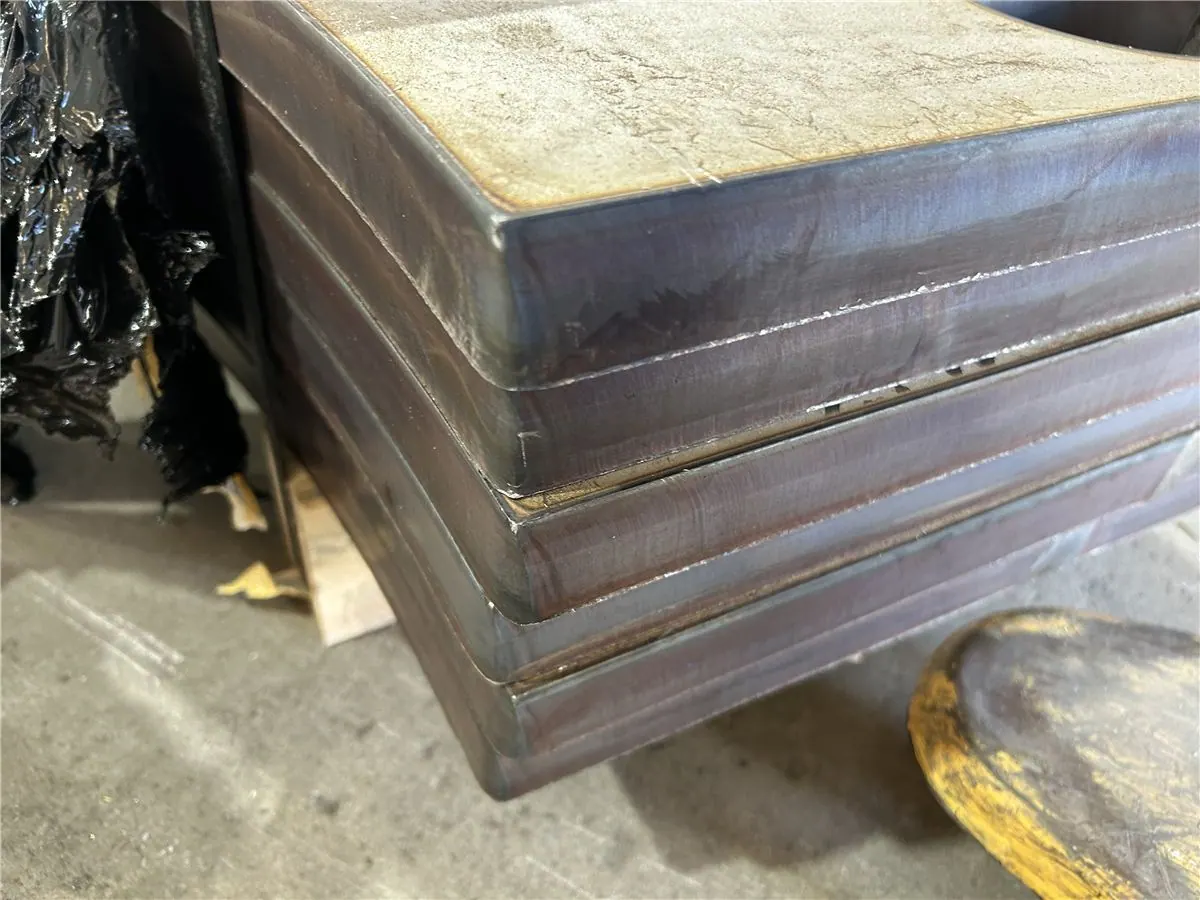
This week at ECI we have completed the first manufacturing stage of a set of three units of an alternator turbine plate backing ring.
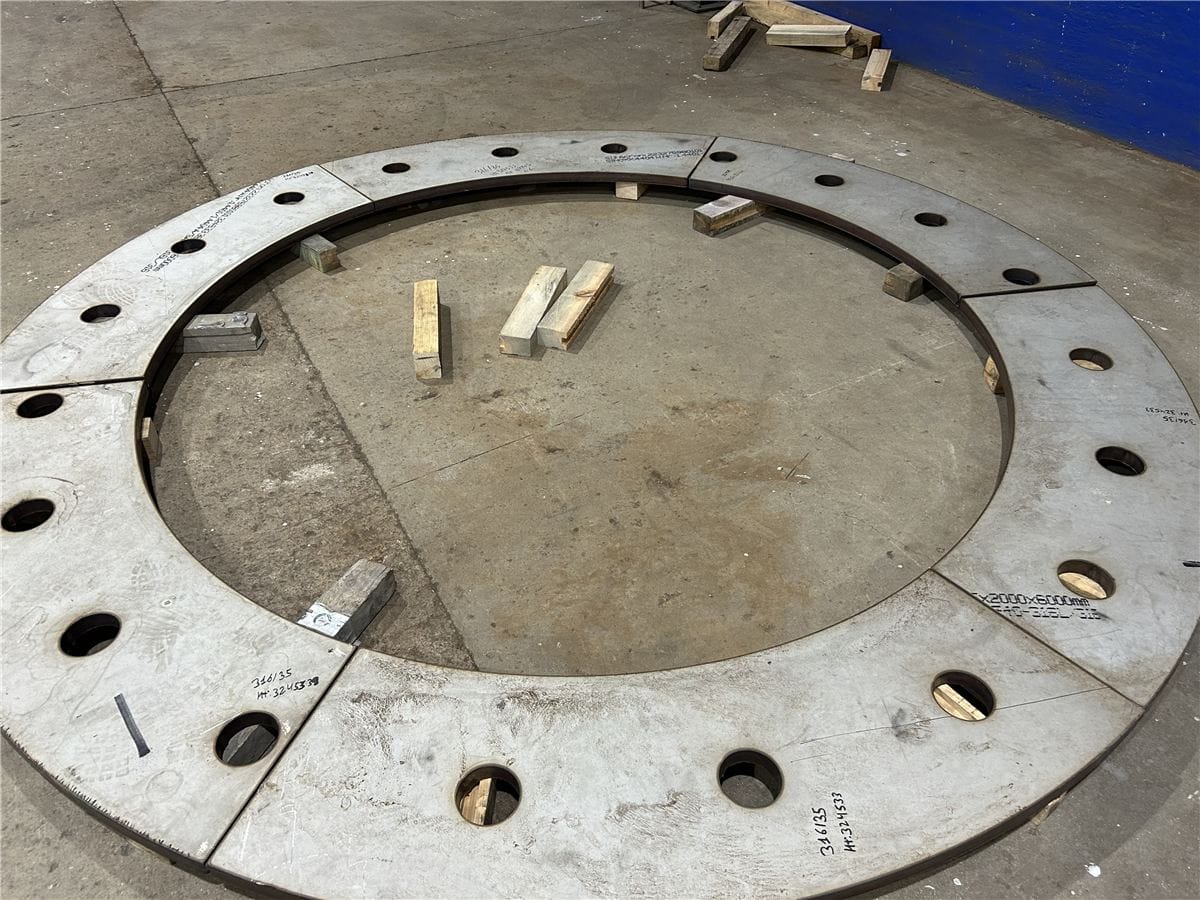
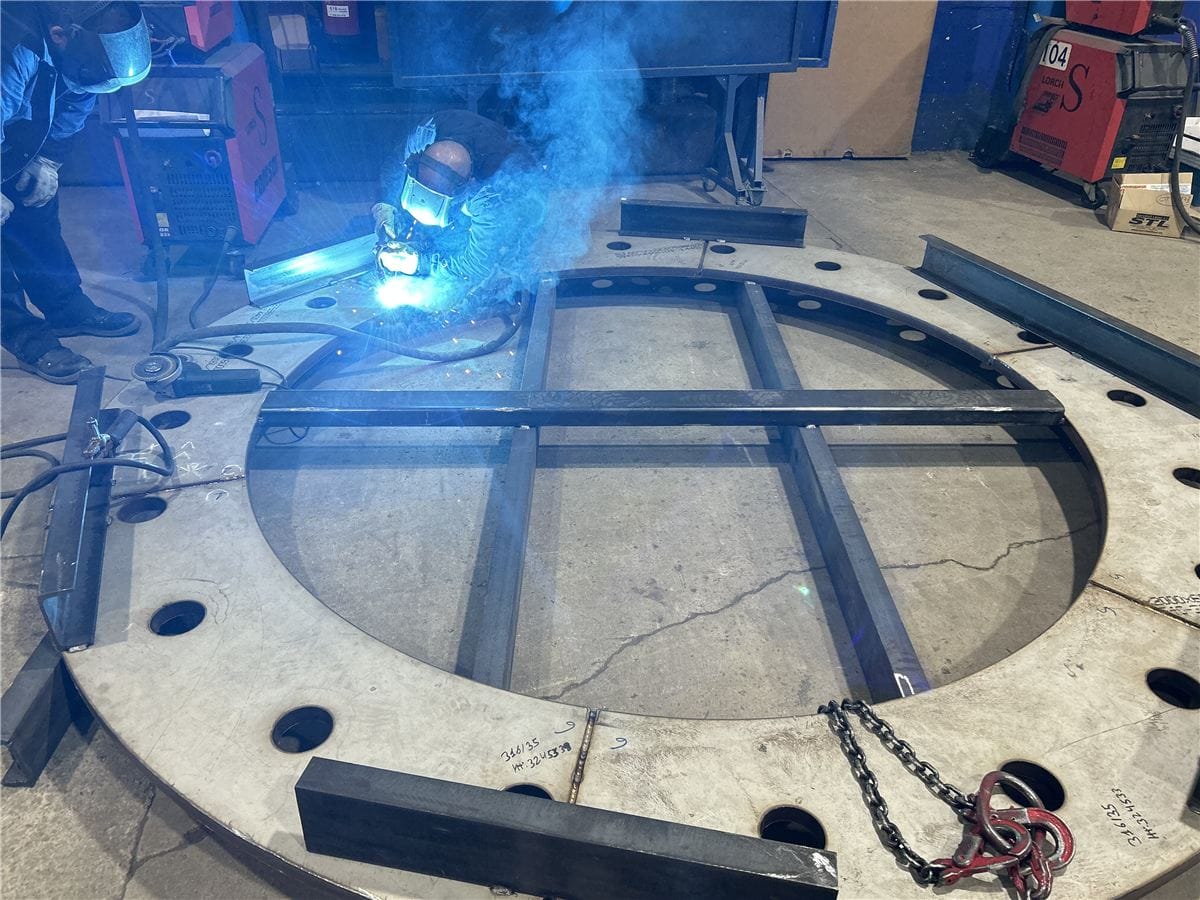
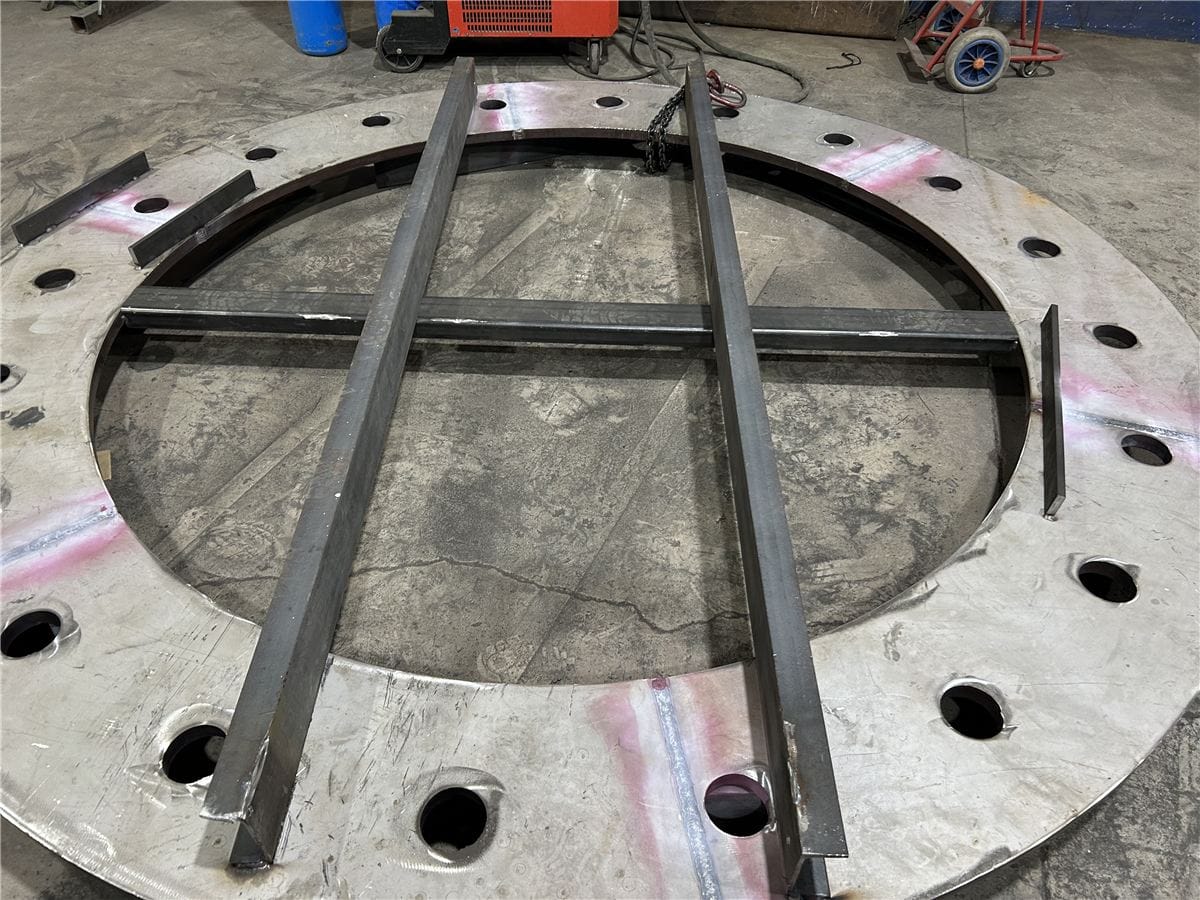
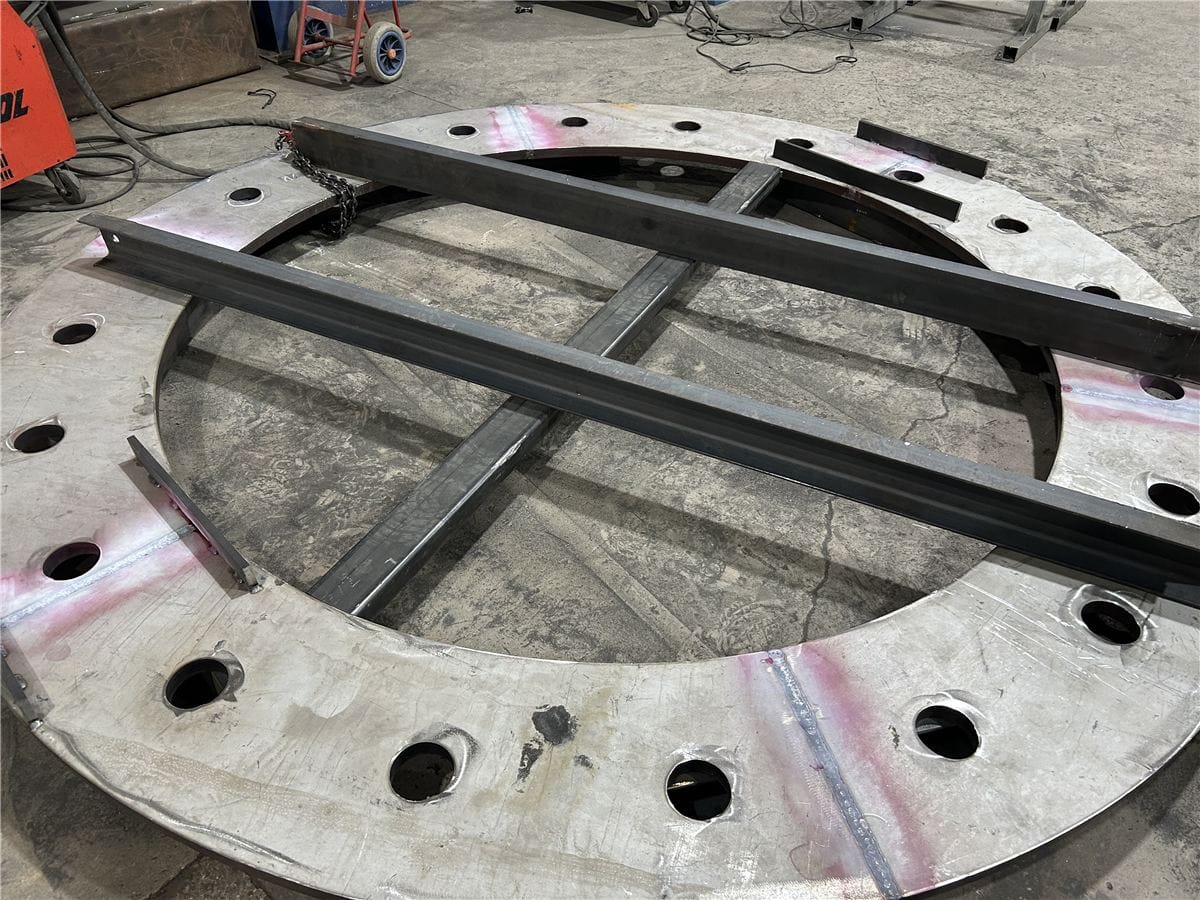
It is a ring with an outside diameter of 3.6 metres and an inside diameter of 2.8 metres, made from six circular sectors of 40 mm thickness each, using high-quality stainless steel (AISI 316-L).
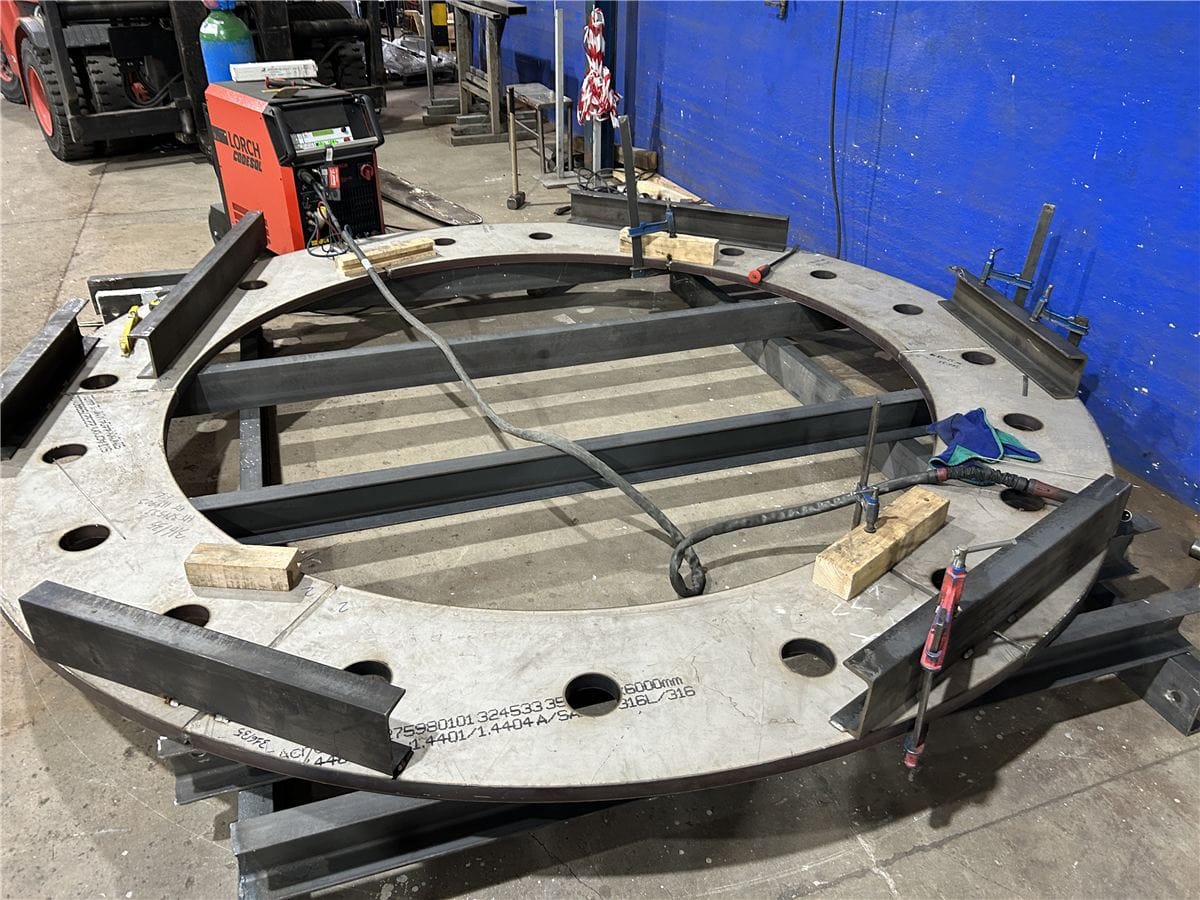
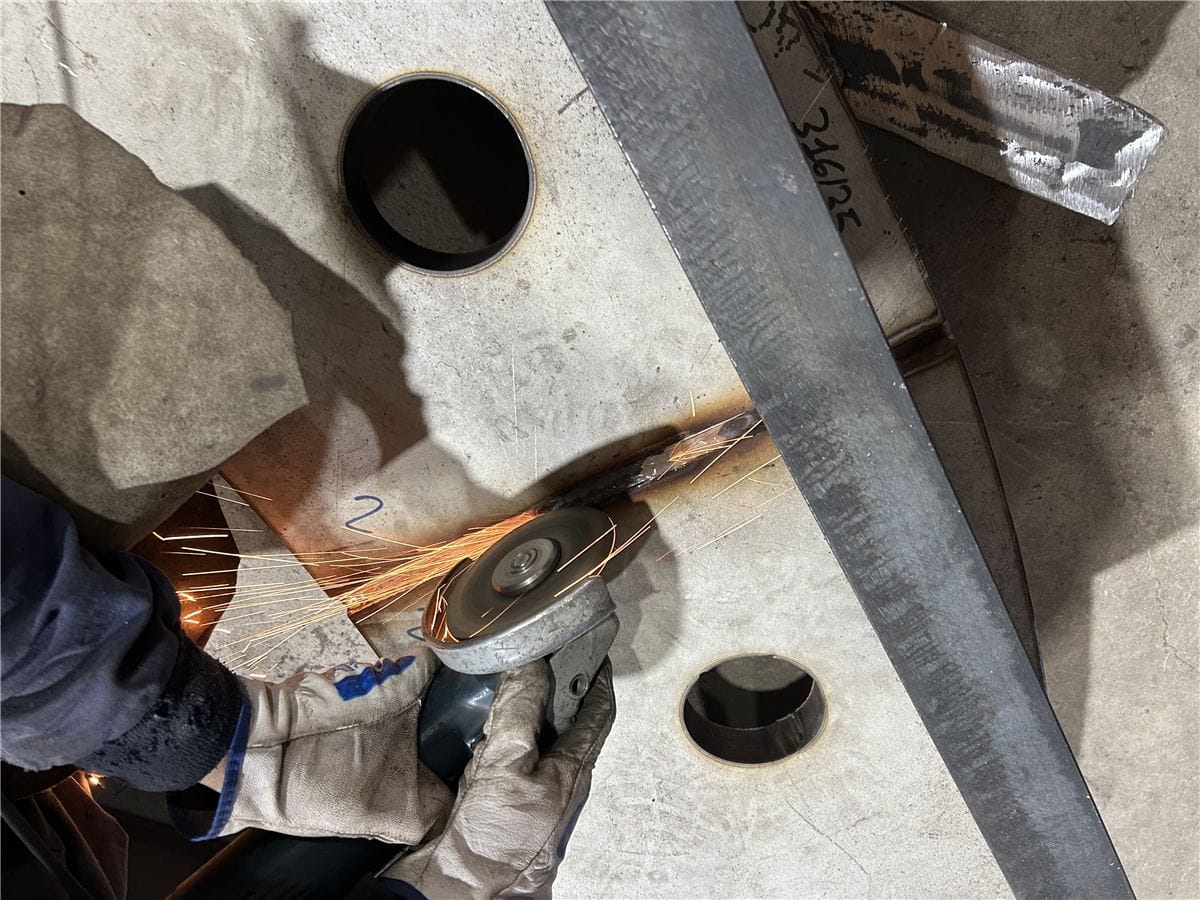
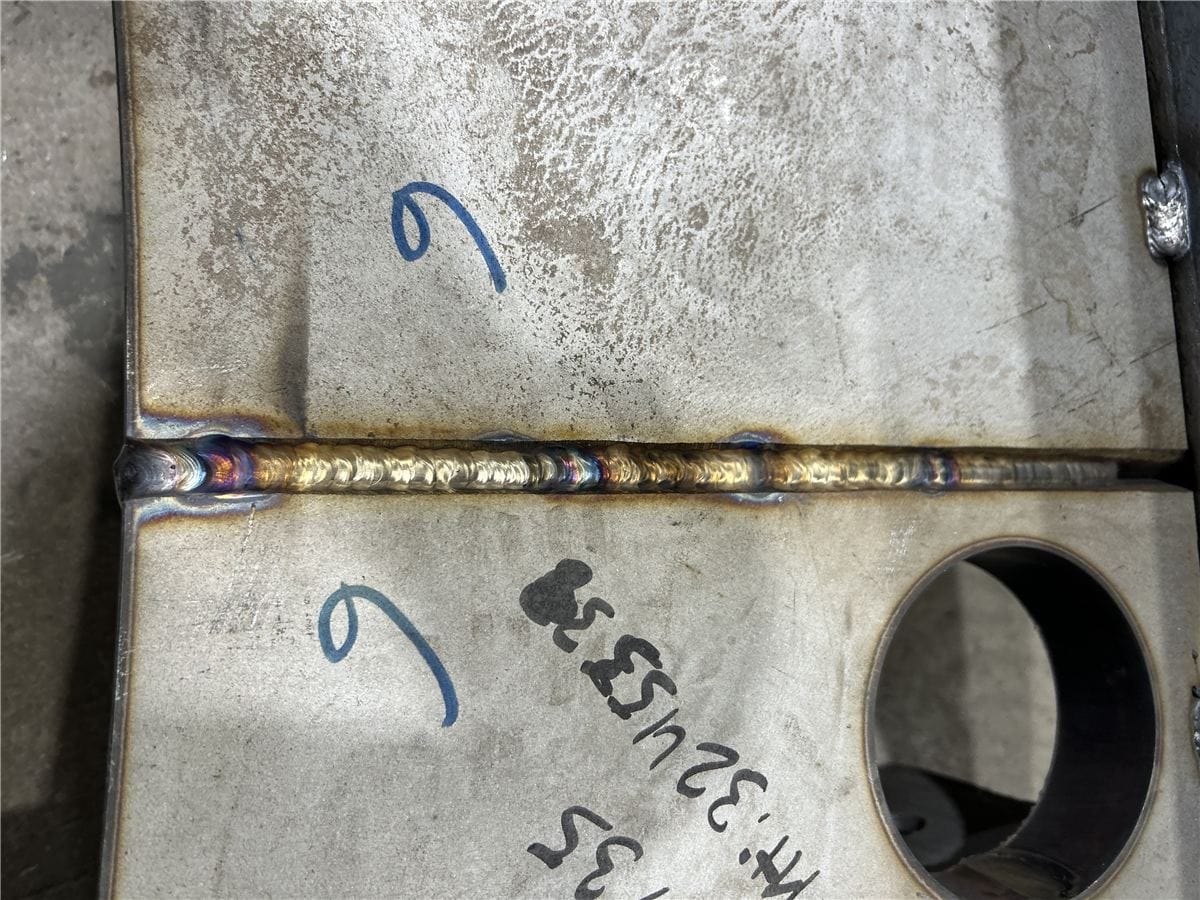
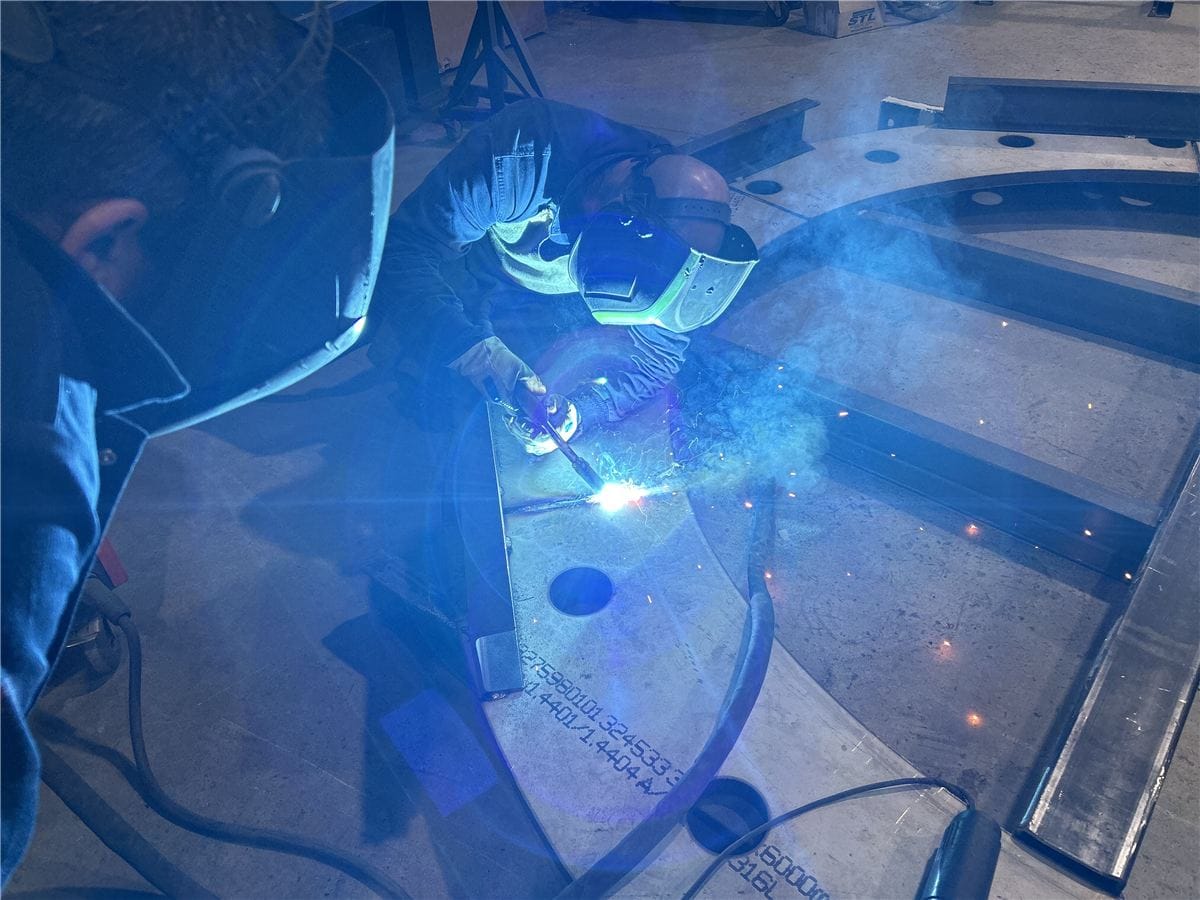
To join these sectors, six multi-pass “X”-shaped butt welds (BW) with full penetration were made. The first two passes were done with TIG (141) and the following ones with MIG (136) using flux-cored wire with inert gas.
Given its vital function once fitted to the alternator of the hydroelectric power plant, strict quality controls were applied, including ultrasonic inspection of the base material, flatness checking of each sector, ultrasonic inspection of the welds, surface inspection with penetrant liquids and visual control.
Before machining, the ring was put through a heat-treatment furnace to remove the stresses caused by welding. Finally, a dimensional and flatness check was carried out before it was transported to the machine shop to complete the manufacturing process and proceed to assembly on the plant’s first alternator.
This has been an exhaustive process in which every member of the team has done their job exceptionally well, and we are therefore very pleased. We are getting ready to start manufacturing the next set.
Below are photos showing the results of this successful project: